
FIELD CASE · CNC MACHINE TOOLS
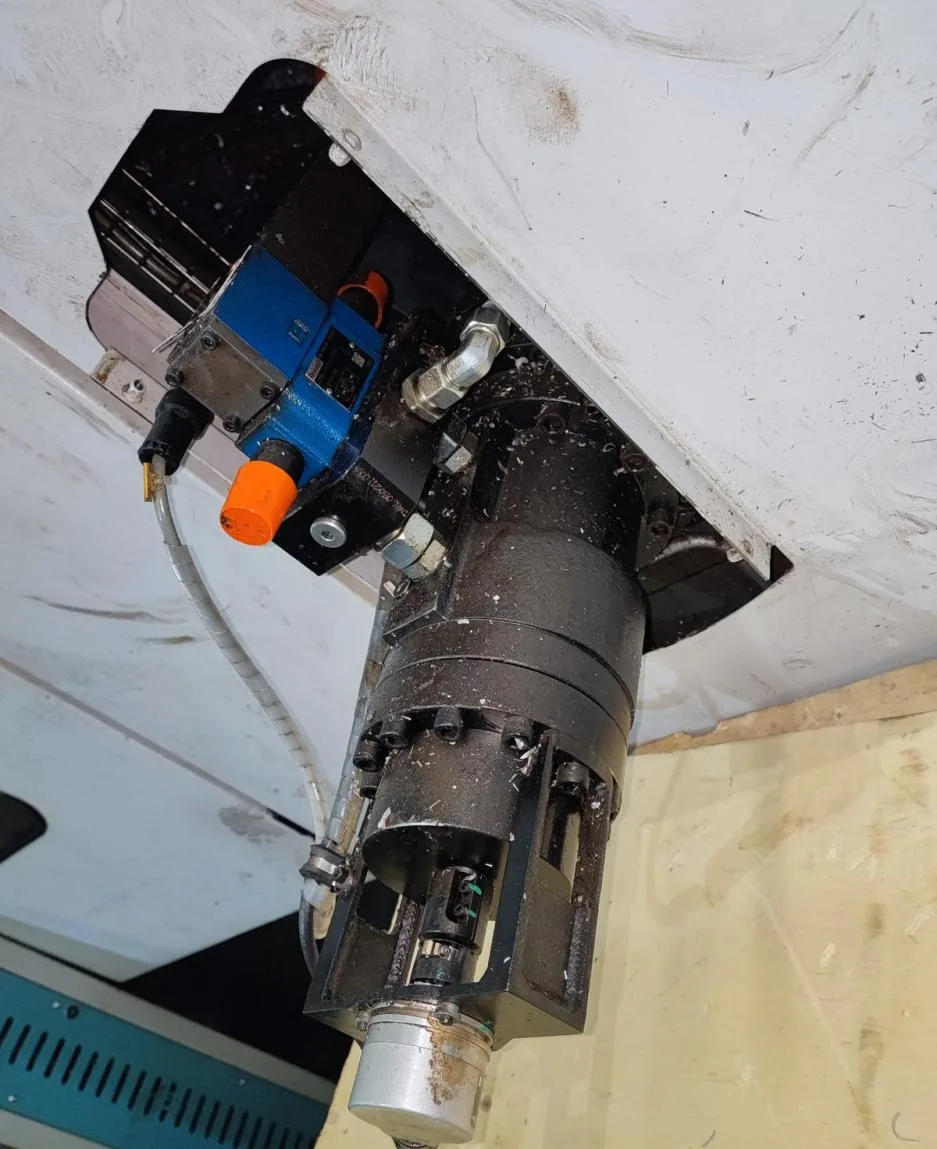
Rotary actuator on a horizontal machining centre tilting table
An independently engineered helical rotary actuator, installed in October 2021 on a Vigel-class machining centre in China, indexing the tilting worktable through 182°±1° at 210 bar — in continuous production service with no reported actuator failure to date.
Documented as an in-service validation record. Identification references to the original equipment are used for compatibility only; HM Hydraulics is an independent supplier.
THE APPLICATION
A demanding indexing duty on a production machine
Horizontal machining centres use a compact helical rotary actuator to tilt and index the worktable. The duty combines high hydraulic pressure, repeated torsional reversals and a tight angular tolerance — on a machine that is expected to run for years without unplanned stops.
Application
Tilting (trunnion) worktable drive on a horizontal machining centre
Actuator type
Helical rotary actuator
Index angle
182° ±1°
Max. working pressure
210 bar
Nominal torque
2,500 Nm
Platform reference
DA-H 100 envelope / D.SWZ S4117 class
Installed
October 2021
Service status
In continuous production; no reported actuator failure to date
FIELD BACKGROUND
Repeated piston cracking on earlier units
A Chinese manufacturer operating machining centres of this platform (originally commissioned in 2016) reported two rotary-actuator failures within a single month during normal production. In both units the internal piston body had cracked.
The reported failure mode was fatigue of the monolithic bronze-alloy piston under repeated torsional and hydraulic loading at operating speed. End-stop damping was checked and found to be within its normal range, and no external mechanical overload was identified; the machine had run without incident for several years beforehand.
We describe the observed failure mode factually and make no claim about the general quality or design of any original-equipment manufacturer's product. Failure causes are application-specific and are confirmed per unit.
THE HM HYDRAULICS BUILD
Engineered to the same interface, built for the load cycle
Piston material upgrade
The piston is specified in an upgraded material and heat-treatment to remove the bronze-alloy cracking mode observed in the failed units under cyclic torsional and hydraulic loading.
Matched envelope and bolt pattern
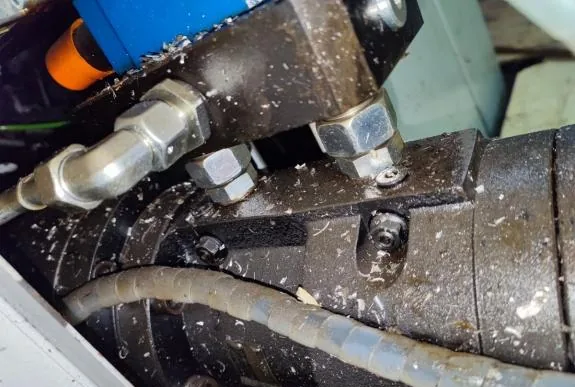
Built to the same external envelope and mounting-bolt pattern for the platform. Fit is confirmed against the individual machine drawing rather than assumed from a catalogue match.
Valve and sensor compatibility
Designed to work with the existing hydraulic valve assembly and position sensors already on the machine, avoiding changes to the control and hydraulic systems.
Rated to the duty
Rated to 210 bar working pressure for the 182°±1° tilting index, with every actuator pressure-tested before shipment.
RESULT
Installed October 2021 — continuous production service, no reported actuator failure
The platform has since been supported with repeat and batch builds. The record reflects this specific installation and duty cycle; results vary with application and maintenance.
HOW WE QUALIFY A REPLACEMENT
Verified per unit, not assumed from a code
1. Nameplate & drawing review
We confirm the actuator model, index angle, pressure rating, bolt pattern and port/valve arrangement against the unit nameplate and the machine mounting drawing before quoting.
2. Engineering match
We select or adapt a build to the same envelope and interface, and confirm compatibility with the existing valve assembly and position sensing on the machine.
3. Build & pressure test
Every actuator is pressure-tested before shipment; piston and housing materials are specified for the cyclic torsional and hydraulic loads of the duty cycle.
4. Fit verification & supply
Fit is verified on the actual machine. Once accepted, we support service units, repeat builds and batch supply for the platform.
Questions
Is this an original HKS or Vigel part?+
No. HM Hydraulics supplies an independently engineered alternative unit. HKS, Vigel, Rexroth and any model/order numbers referenced on this page are the property of their respective owners and are used only for identification and compatibility reference. We do not represent the unit as an original part or imply affiliation with, or endorsement by, those companies.
Does it fit a DA-H 100 / D.SWZ S4117 directly?+
In the documented installation the unit was built to the same external envelope and mounting-bolt pattern and used the existing valve assembly and position sensors. Because machines differ by build year and configuration, we verify the interface against your specific unit nameplate and mounting drawing before confirming any replacement.
What operating data supports the case?+
The actuator was installed in October 2021 on a Vigel-class horizontal machining centre in China for the tilting-worktable axis at 210 bar and a 182°±1° index, and has remained in continuous production service with no reported actuator failure. The figures describe this specific installation and are not a generalised warranty or service-life guarantee.
How do I get the specification sheet and mounting drawing?+
Send the model tag, part number and a photo of your mounting face, shaft and machine nameplate using the form below or email bai@hmhydraulics.com. We provide the full specification, engineering drawing and quality documentation for your engineering team to review.
ENGINEERING PACK ON REQUEST
Get the specification sheet and mounting drawing
Full dimensional drawing, torque/pressure curves, port and valve details and quality documentation are provided for your engineering team to review — on request, not posted publicly.
Send the model tag, part number and photos of the mounting face, shaft and machine nameplate. We confirm the interface against your exact unit and return the matching build and documents.
Or email Kevin Bai directly at bai@hmhydraulics.com.